


Overview
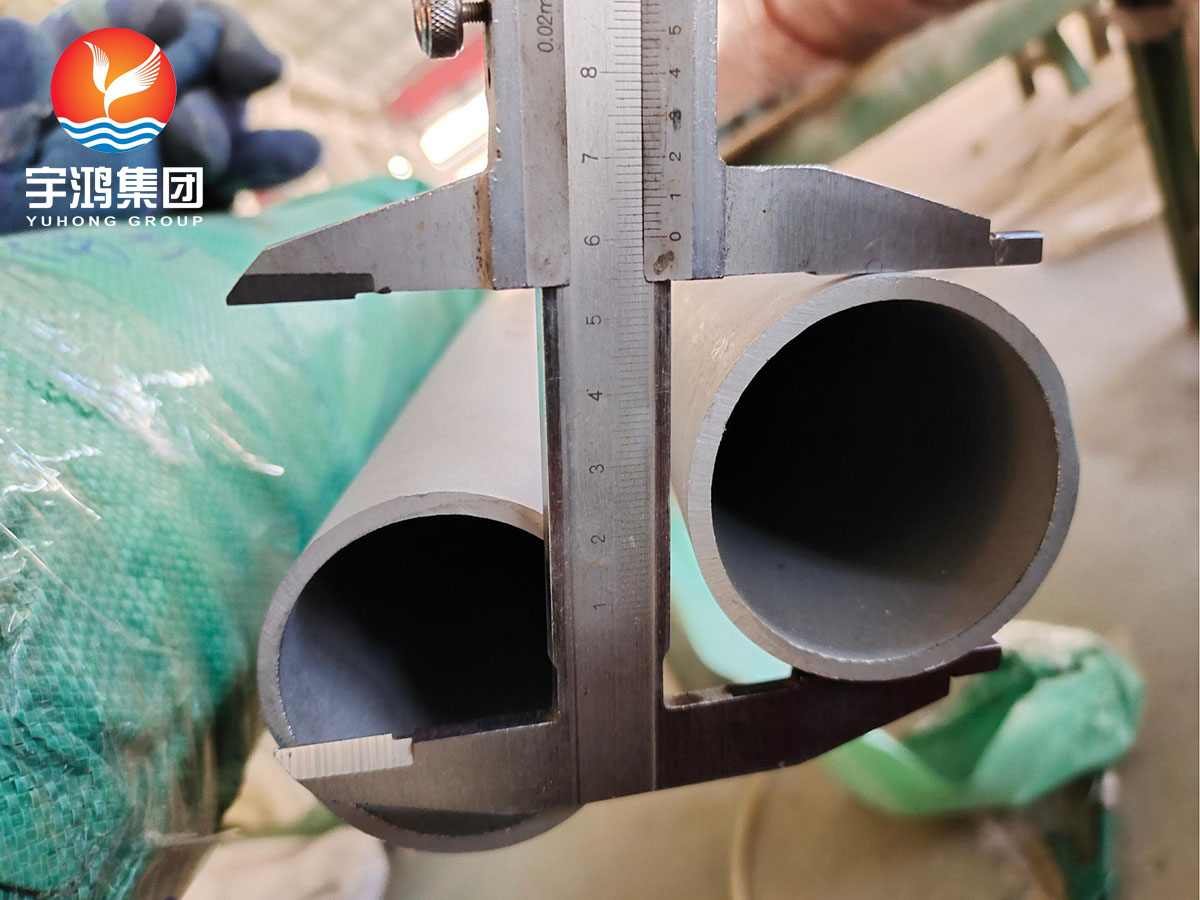
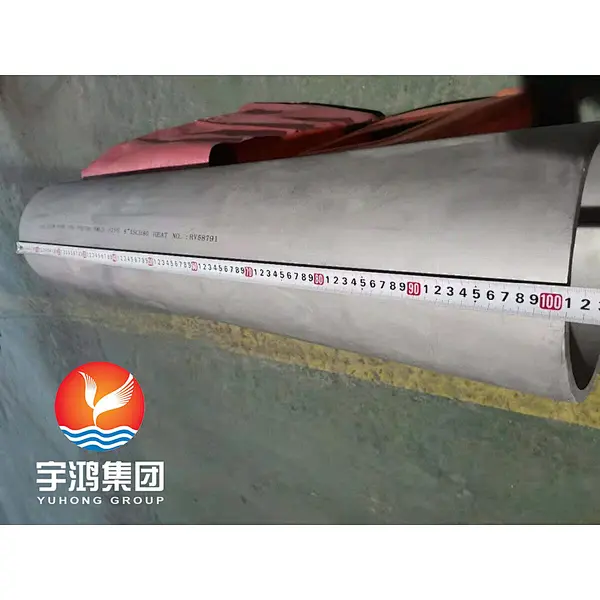
The ASTM A790 S32750 Super Duplex Steel Welded Pipe is a welded pipe manufactured from super duplex stainless steel UNS S32750 (commonly known as 2507), with a balanced austenitic-ferritic microstructure. Through its high-alloy formulation of 25%Cr + 7%Ni + 4%Mo + 0.3%N, S32750 achieves a Pitting Resistance Equivalent Number (PREN) of ≥40, a Critical Pitting Temperature exceeding 50°C, and a yield strength approximately twice that of 316L.
Our A790 S32750 welded pipes are produced using advanced welding processes (PAW+GTAW or DC TIG) and delivered in the solution annealed + pickled condition, with dimensions conforming to ASME B36.19 and B36.10. They are specifically designed for seawater cooling systems, offshore platforms, subsea manifolds, desalination plants, and chemical processing applications.
Related Specifications of S32750
- F53
- Sandvik SAF 2507®*
- NACE MR 0175
- ISO 15156-3
- NORSOK M-630
- 1.4410
- X2CrNiMoN25-7-4
UNS S31803 (F51), UNS S32205 (F60) Alloy 2205, UNS S32550 (F61), UNS S32750 (F53), Alloy 2507 and UNS S32760 (F55).
Standards: ASTM/ASME A789/SA789, A790/SA790, A450, A530.
Material: UNS S31803(Cr22Ni5Mo3/1.4462)/2205, UNS S32750(1.4410), UNS S31500(Cr18NiMo3Si2), UNS32760(1.4501).
Chemical Composition
Grade | C max | Si max | Mn max | P max | S max | Cr | Ni | Mo | N |
UNS S32750 | 0.030 | 0.8 | 1.2 | 0.030 | 0.015 | 24.0-26.0 | 6.0-8.0 | 3.0-5.0 | 0.24-0.32 |
UNS S31803 | 0.030 | 1.0 | 2.0 | 0.020 | 0.020 | 21.0-23.0 | 4.5-6.5 | 2.5-3.5 | 0.08-0.20 |
UNS S31500 | 0.030 | 1.0 | 1.2-2.0 | 0.030 | 0.030 | 18.0-19.0 | 4.5-5.5 | 2.5-3.5 | 0.05-0.10 |
Nitrogen (N) is the key element distinguishing S32750 from standard duplex grades. The 0.24–0.32% nitrogen content significantly enhances pitting resistance while pushing yield strength to the 550 MPa level.
Physical Properties
Grade | Y.S.MPa min | T.S.Mpa min | Elongation % | Hardness HRC |
UNS S32750 | 550 | 800 | 15 | 20 |
UNS S31803 | 450 | 620 | 25 | 20 |
UNS S31500 | 440 | 630 | 30 | 20 |
Yield strength is approximately twice that of 316L, allowing designers to reduce wall thickness in pressure-bearing applications, lowering weight and cost.
Weld Quality Requirements
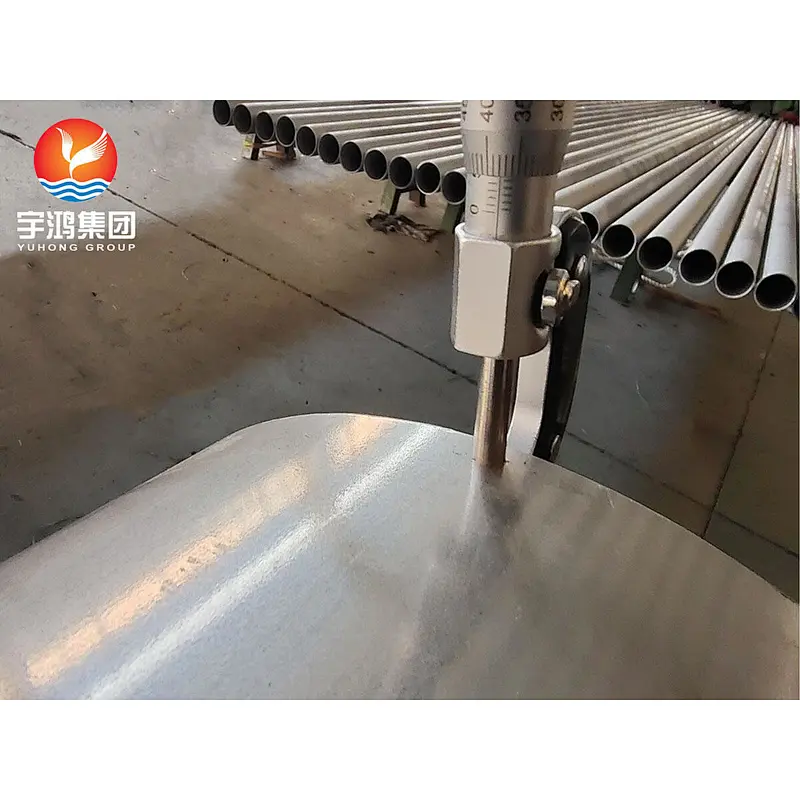
Research on Φ50.8 mm × 0.89 mm ultra-light-wall S32750 welded pipe using DC TIG process demonstrated:
Weld seam zone composed of uniformly distributed ferrite and austenite
Hardness of weld, HAZ, and base metal ≤ 300 HBW, with hardness difference controlled within 15 HBW
Good weld formation without defects such as undercut
Comparison with Other Common Materials
S32750 vs S32205 (2205) Duplex
| Comparison Dimension | S32750 (2507) | S32205 (2205) |
|---|---|---|
| PREN | ≥ 40 | 34–36 |
| Critical Pitting Temperature | >50°C | 35–45°C |
| Yield Strength | ≥ 550 MPa | ≥ 450 MPa |
| Seawater Service Temperature | Up to approx. 50°C | Ambient only |
| Cost | Higher | Lower |
Selection Principle: For seawater service above 40°C, NACE MR0175 sour gas compliance, or subsea high-salinity warm water, S32750 is required. For ambient seawater and general chloride environments, 2205 offers a cost-effective alternative.
S32750 vs 6Mo Super Austenitic (254 SMO)
| Comparison Dimension | S32750 | 254 SMO |
|---|---|---|
| Yield Strength | ≥ 550 MPa | ≥ 300 MPa |
| PREN | ≥ 40 | ≥ 42 |
| Chloride SCC Resistance | Excellent | Excellent |
| Weldability | More challenging | Easier |
S32750 offers significantly higher strength than 6Mo super austenitic grades, allowing thinner wall designs, but requires more stringent welding controls.
Typical Application Scenarios
Offshore Oil and Gas: Subsea umbilicals, FPSO piping, seawater cooling systems, offshore platform process piping
Seawater Desalination: Reverse osmosis (RO) desalination piping, brine systems
Chemical Processing: Chloride-containing media, organic acid piping, heat exchangers
Subsea Manifolds: Deepwater manifold piping (validated for 1000m subsea service)
Pulp and Paper: Bleach plant piping, chlorine dioxide systems
Common Specification Reference
| Parameter | Common Range |
|---|---|
| Outer Diameter | 6.35 mm – 273.1 mm (1/8"– 10"NB) |
| Wall Thickness | 0.5 mm – 50 mm |
| Length | Up to 18 meters |
| Schedules | 5S, 10S, 20, 40S, 80S, 160, XXS |
| End Finish | Plain End, Beveled, Threaded & Coupled |
| Delivery Condition | Solution annealed + pickled & passivated |
We can provide custom sizes, schedules, and end finishes per customer requirements, with hydrostatic testing, eddy current testing, UT for weld seam, and ASTM A923 corrosion testing available.
Quality Assurance and Services
Standard Compliance: Strictly manufactured to ASTM A790 / ASME SA790, with EN 10204 3.1/3.2 material certificates available
NDT: Hydrostatic test or eddy current; UT for weld seam
Corrosion Testing: ASTM A923 Method A/B/C available; many EPC specifications require Method C (ferric chloride corrosion test)
Heat Treatment Control: Solution annealing at 1050–1125°C + rapid water quenching, ensuring ferrite content 40–60%
Customization Services: Drawing-based customization of sizes, schedules, and end finishes
Technical Support: Assistance with confirming S32750 applicability based on customer media chloride concentration and temperature conditions
FAQ
Q1: Are S32750, 2507, and F53 the same material?
Yes. S32750 is the UNS unified numbering system designation, 2507 is the commercial trade name (originally Sandvik SAF 2507), and F53 is the ASTM A182 forging grade designation. The EN designation is 1.4410.
Q2: What is the difference between ASTM A790 and ASTM A928?
A790 covers seamless and welded duplex pipe without filler metal (autogenous welding). A928 covers duplex pipe electric fusion welded with addition of filler metal. For welded pipe made with filler metal from plate, A928 applies.
Q3: What is the maximum service temperature of S32750?
300°C is the typical maximum service temperature for S32750 super duplex steel. Above this temperature, the material embrittles due to sigma phase precipitation. The recommended continuous service temperature range is -40°C to 250°C.
Q4: What ferrite content is required for S32750 welded pipe?
The ferrite content should be controlled within 40–60%. Too high (>70%) decreases toughness and pitting resistance; too low (<25%) decreases SCC resistance. Ferrite content is typically measured on the weld seam to verify proper welding and annealing.
Q5: What welding filler metal is recommended for S32750?
ER2594 is the recommended matching composition filler metal. For autogenous welding (no filler), the PAW+GTAW process is commonly used.
Q6: What is the ASTM A923 corrosion test?
ASTM A923 is a test method to detect detrimental intermetallic phases (sigma, chi) in duplex stainless steels. Method A is sodium hydroxide etch, Method B is Charpy impact, and Method C is ferric chloride corrosion test. Many EPC project specifications require Method C (the most stringent) for all duplex pipe.
Q7: Is S32750 suitable for sour gas service?
Yes. S32750 with PREN ≥ 40 meets NACE MR0175 / ISO 15156 requirements for sour gas service. It is widely used in subsea manifolds, inlet separators, and slug catchers in sour gas processing systems.
Q8: What are the delivery lead time and minimum order quantity?
Delivery lead time and minimum order quantity are determined by specifications, quantity, and testing requirements. Common specifications are available from stock; custom specifications typically require 15–30 working days. Please consult our sales team for details.