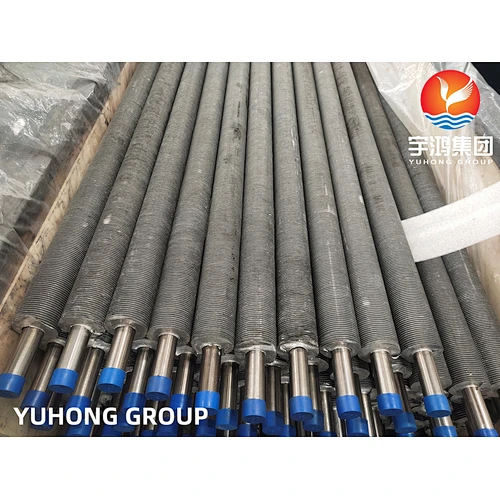
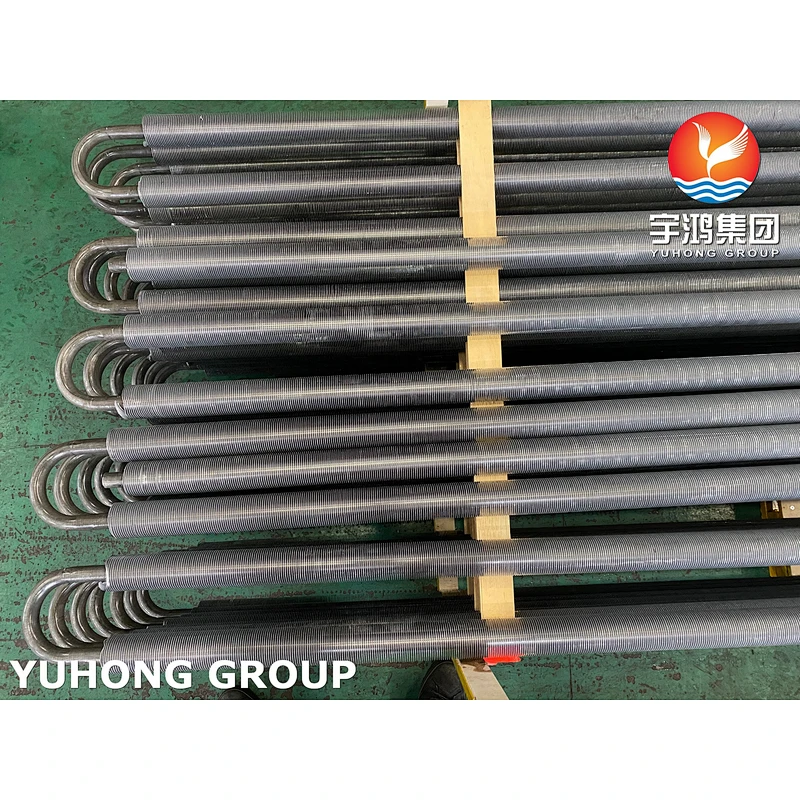
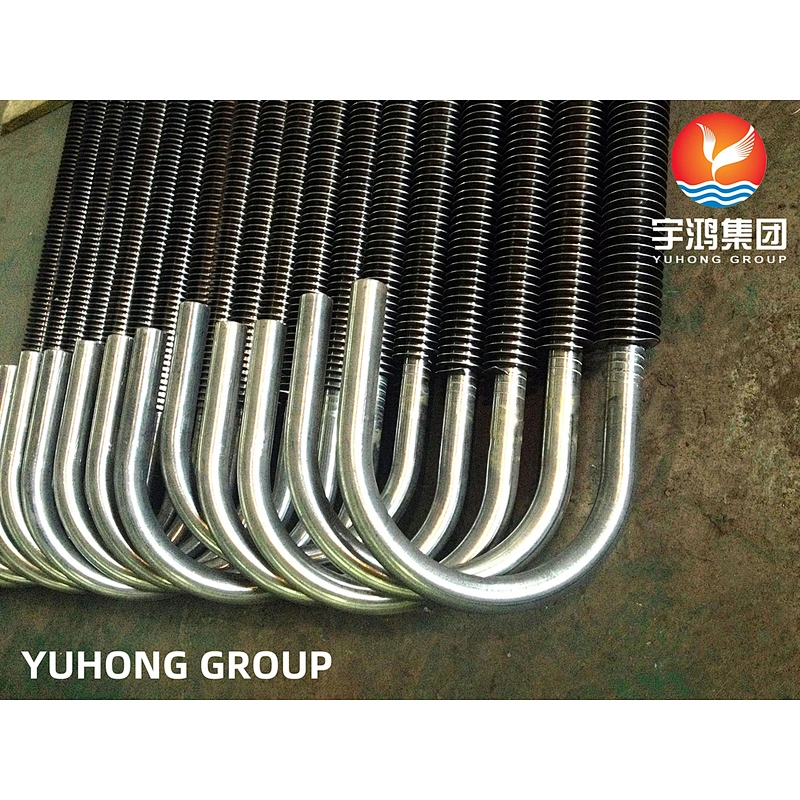
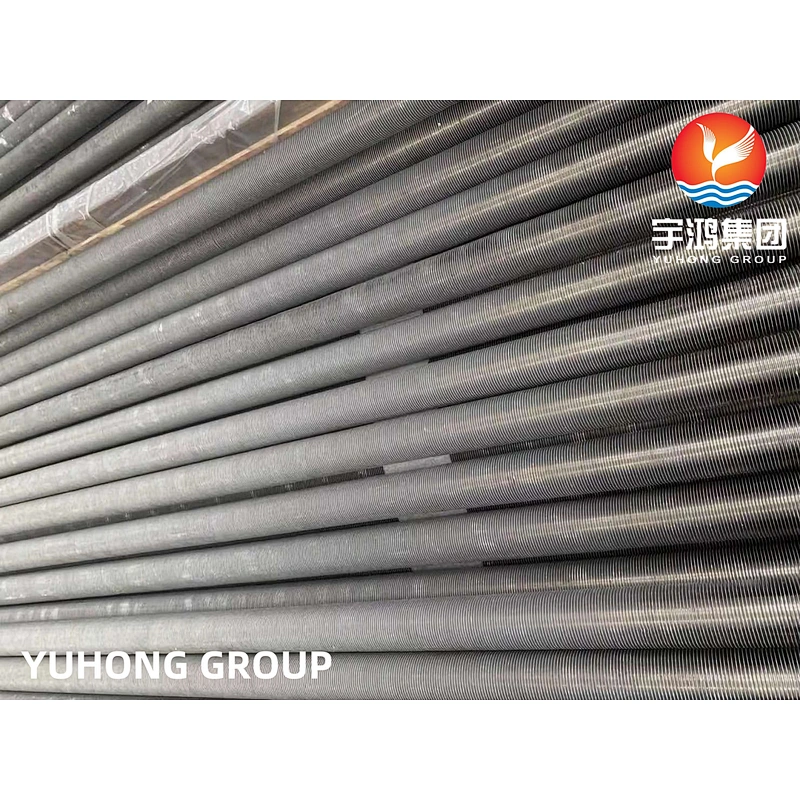
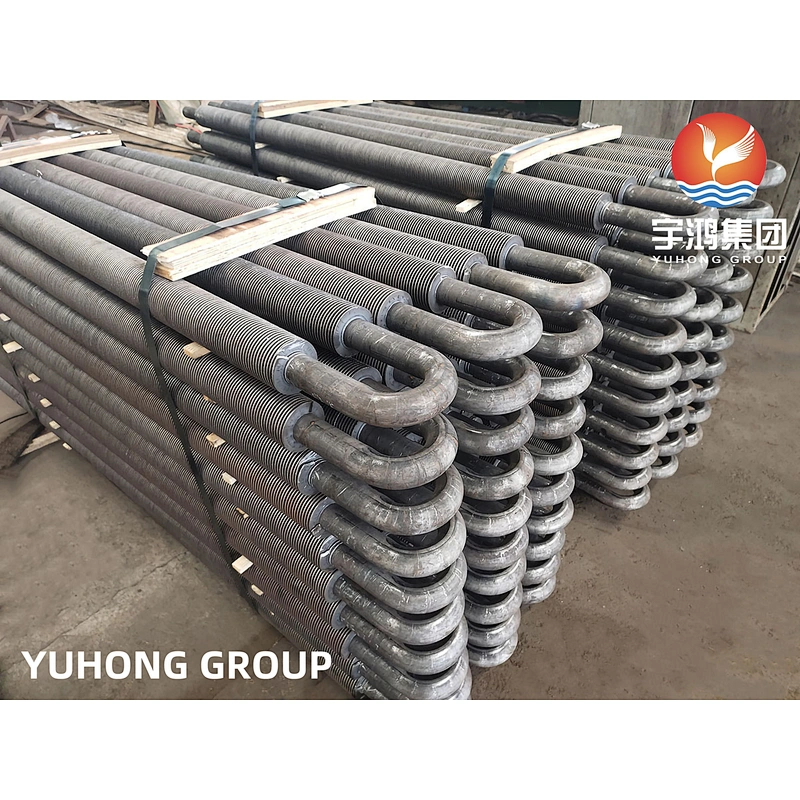

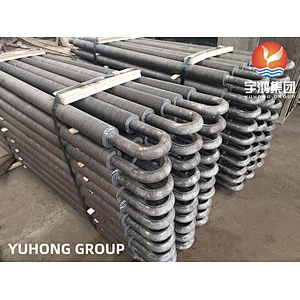
STAINLESS STEEL U BEND FINNED TUBE SPIRAL EXTRUDED/STUD
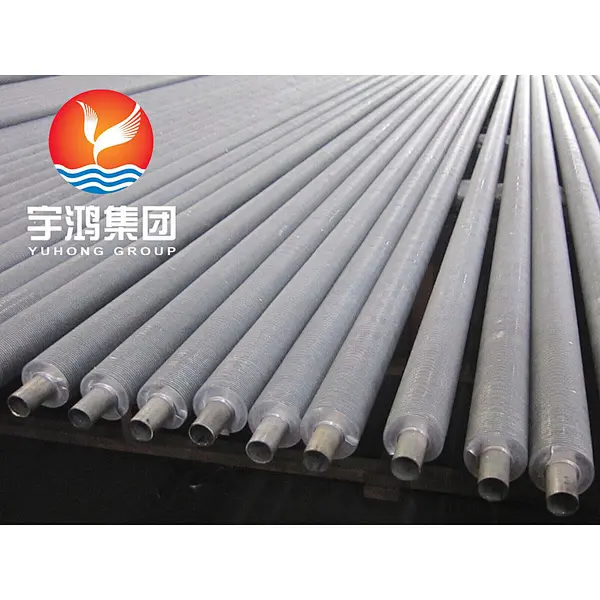
HFW Solid Finned Tubes short for High Frequency Welded Helical Spiral Solid Finned Tube
Helical Finned Tubes provide the designer with high thermal efficiency and compact design solutions for a whole range of heat exchangers where clean flue gases are used. Helical finned Tubes are manufactured in both Solid and Serrated type.
Helical Solid Finned Tubes are manufacturer by helically wrapping continuous fin strip on tube. HF Resistance Welding Usually Employs Frequency Of 400 kHz. The fin wound around the tube And Continuous weld. The fin strip is wounded spirally onto the tube and welded continuously with a high frequency electrical process to the base tube along the spiral root. The fin strip held under tension and confined laterally as it is formed around the tube, thereby ensuring that the strip is in forceful contact with the base tube surface. A continuous weld is applied at the point where the fin strip first begins to bend around the tube diameter, using the gas metal arc welding process.
For a given tube or pipe size, the desired heat transfer surface area per unit length of tube can be obtained by specifying the appropriate fin height, fin thickness and /or number of fins per meter of length.
HFW Solid Finned Tube
This welded steel finned tube configuration can be used for any practically heat exchanger application, and is particularly suited to high temperature and high pressure applications. The important features of this configuration are efficient, effective bond of fin to tube under all conditions of temperature and pressure, and ability to withstand high fin-side temperatures.
A continuous helical fin is attached to the base tube by high frequency electric resistance welding in order to give an efficient and thermally reliable bond.
Technical Details/Base Tube Details
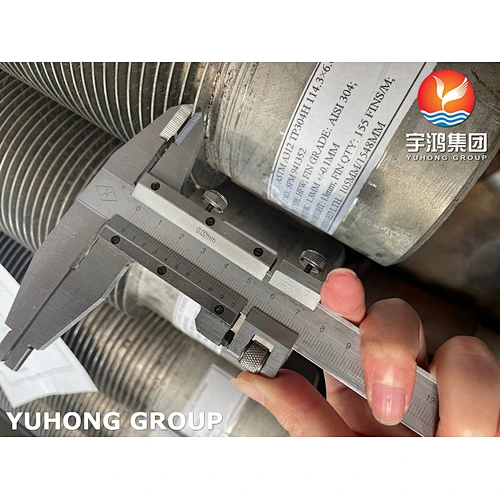
Tube Diameter : 20 mm OD Min to 219 mm OD Max.
Tube Thickness : Minimum 2 mm up to 16mm
Tube Material : Carbon Steel, Stainless Steel, Alloy Steel, Corten steel, duplex Steel, Super Duplex Steel, Inconel, High Chrome High Nickle & Incolloy, CK 20 material and some other material.
Fin Details
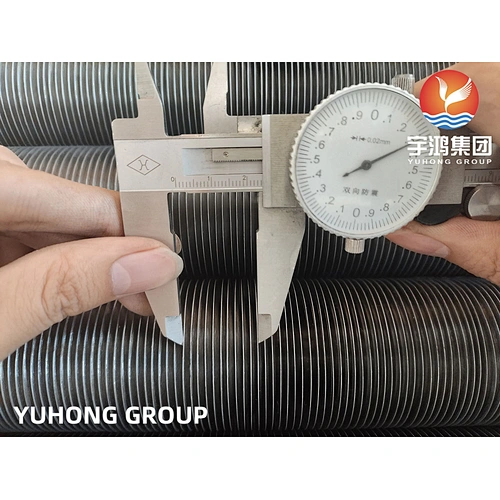
Fins Thickness : Min. 0.8 mm to Max. 4 mm
Fins Height : Min 0.25” (6.35 mm) To Max.1.5” (38 mm)
Fin Density : Min 43 Fins Per Meter To Max. 287 Fins Per Meter
Material : Carbon Steel, Stainless Steel, Alloy Steel, Corten steel, Duplex Steel and Incolloy.
U-Bend Fabrication for Finned Tubes
U-bend fabrication of finned tubes requires specialized equipment and process control to prevent fin damage and maintain tube integrity:
Bending Process
The U-bend is formed using a multi-stage bending method with a pair of left/right bending rolls and a rotary/elevating pressure die. The finned tube is intermittently fed for a certain length, and U-shaped bends are formed alternately. For multi-stage serpentine bending, the tube is rotated downward from the horizontal state and inclined at a predetermined angle after each stage of bending.
Key Considerations
Fin Clearance: The bending apparatus must accommodate the fin height to avoid crushing or deformation
Wall Thinning Control: Outer wall thinning should be controlled, typically within 15–20% depending on bend radius
Fin Integrity: Extruded fins, being robust and metallurgically bonded, generally withstand bending better than wrapped fins
Comparison with Other Finned Tube Types
| Fin Type | Bond Method | Max Temp | Fin-to-Tube Contact | Best For |
|---|---|---|---|---|
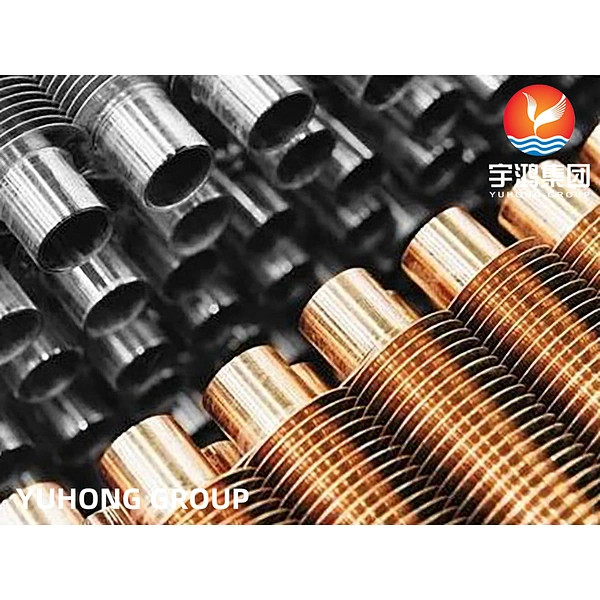
| Extruded | Mechanically solid pressed | ~280°C | 100% | Corrosive atmospheres, best bond |
| L-Foot Wrapped | Interference fit | ~150–250°C | Line contact | Air coolers, economical |
| G-Fin (Embedded) | Rolled into groove | ~400°C | Good mechanical lock | Higher temperature, cyclic duty |
| HF Welded | High-frequency welded | ~400°C+ | Metallurgical | Harsh corrosive, high temp |
Selection Principle: Extruded fins are the default choice when corrosion resistance, fin integrity, and reliable heat transfer are priorities. For higher temperatures (>280°C), G-fin or welded fins are recommended.
Typical Application Scenarios
Oil and Gas: Air-cooled heat exchangers for upstream and midstream service
Power Generation: Heat recovery steam generators (HRSG), economizers
Chemical Processing: Process heaters, coolers with corrosive atmospheres
Refinery: Process heaters where reliable fin bond is critical
Marine/Offshore: Seawater-cooled heat exchangers (with appropriate base tube material)